P-02 / Mold making
Mold making
Plastic injection mold making: 12 steps from quote to finished mold
Chang-Hao develops its own plastic injection molds in 12 steps: quotation, kickoff meeting, CAD design, machining, fitting, mold trial, corrections and quality inspection.
Mold components are machined in Chang-Hao’s own tool room, and since the molding plant and mold shop merged in 2000, mold trials run directly on Chang-Hao’s own presses.
By 昌昊興業 (Chang-Hao) · Updated
01 / Workflow
Mold development in 12 steps
Chang-Hao’s mold development process has 12 steps: after the trial the mold is corrected based on the results, and it is complete once several rounds of adjustment and inspection are done and it meets the customer’s requirements.
01Plan
- 01
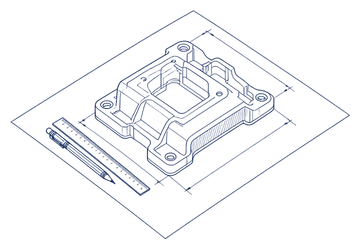
Quotation
Make an initial cost estimate and give the customer a clear budget reference.
- 02
Kickoff meeting
Clarify the customer’s requirements so the team agrees on the project.
- 03
Mold design
Design the mold in CAD to match what the customer expects.
- 04
Production plan
Set the production sequence with efficiency and quality in mind.
- 01
02Build
- 05
Material and drawings
Prepare the material and complete all engineering drawings before machining.
- 06
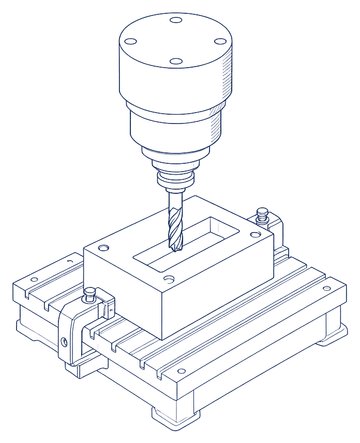
Machining
Machine the mold precisely on CNC machine tools and other equipment.
- 07
Mold fitting
Fit the mold, increasing surface hardness and extending its service life.
- 05
03Verify
- 08
Mold trial
Run a trial before production to confirm how the mold performs.
- 09
Corrections
Modify the mold based on the trial so it meets the customer’s requirements.
- 10
Quality inspection
Inspect every mold to confirm it meets the standards.
- 11
Mold complete
After several rounds of adjustment and inspection, the mold meets the customer’s requirements.
- 08
04Deliver
- 12
Shipment
Start production and deliver to the customer on time.
- 12
02 / Filling
How plastic fills a mold: the gate sets the flow order
During injection, molten plastic enters the cavity through the gate and spreads outward, so the areas farthest from the gate fill last. The fill time plot in Autodesk Moldflow shows exactly this: dark blue at the start of injection and red for the last areas to fill.
When the flow meets a hole it splits into two fronts that rejoin behind it and leave a weld line. Autodesk notes that weld lines are unavoidable when the flow front splits and comes together, around a hole, or with multiple gates; if the last areas to fill are not vented well, air traps are common.
- Gate
- Weld line
- Last to fill
Illustration: flow distance calculated from the part geometry, not a result from mold flow simulation software.
Autodesk Moldflow: Fill time result・Weld and meld lines result・Air traps
03 / Tool room
Tool room equipment
Mold components are machined in Chang-Hao’s tool room; step 6 of the process is precision machining on CNC machine tools and other equipment. The tool room has EDM, milling, turning and surface grinding machines.
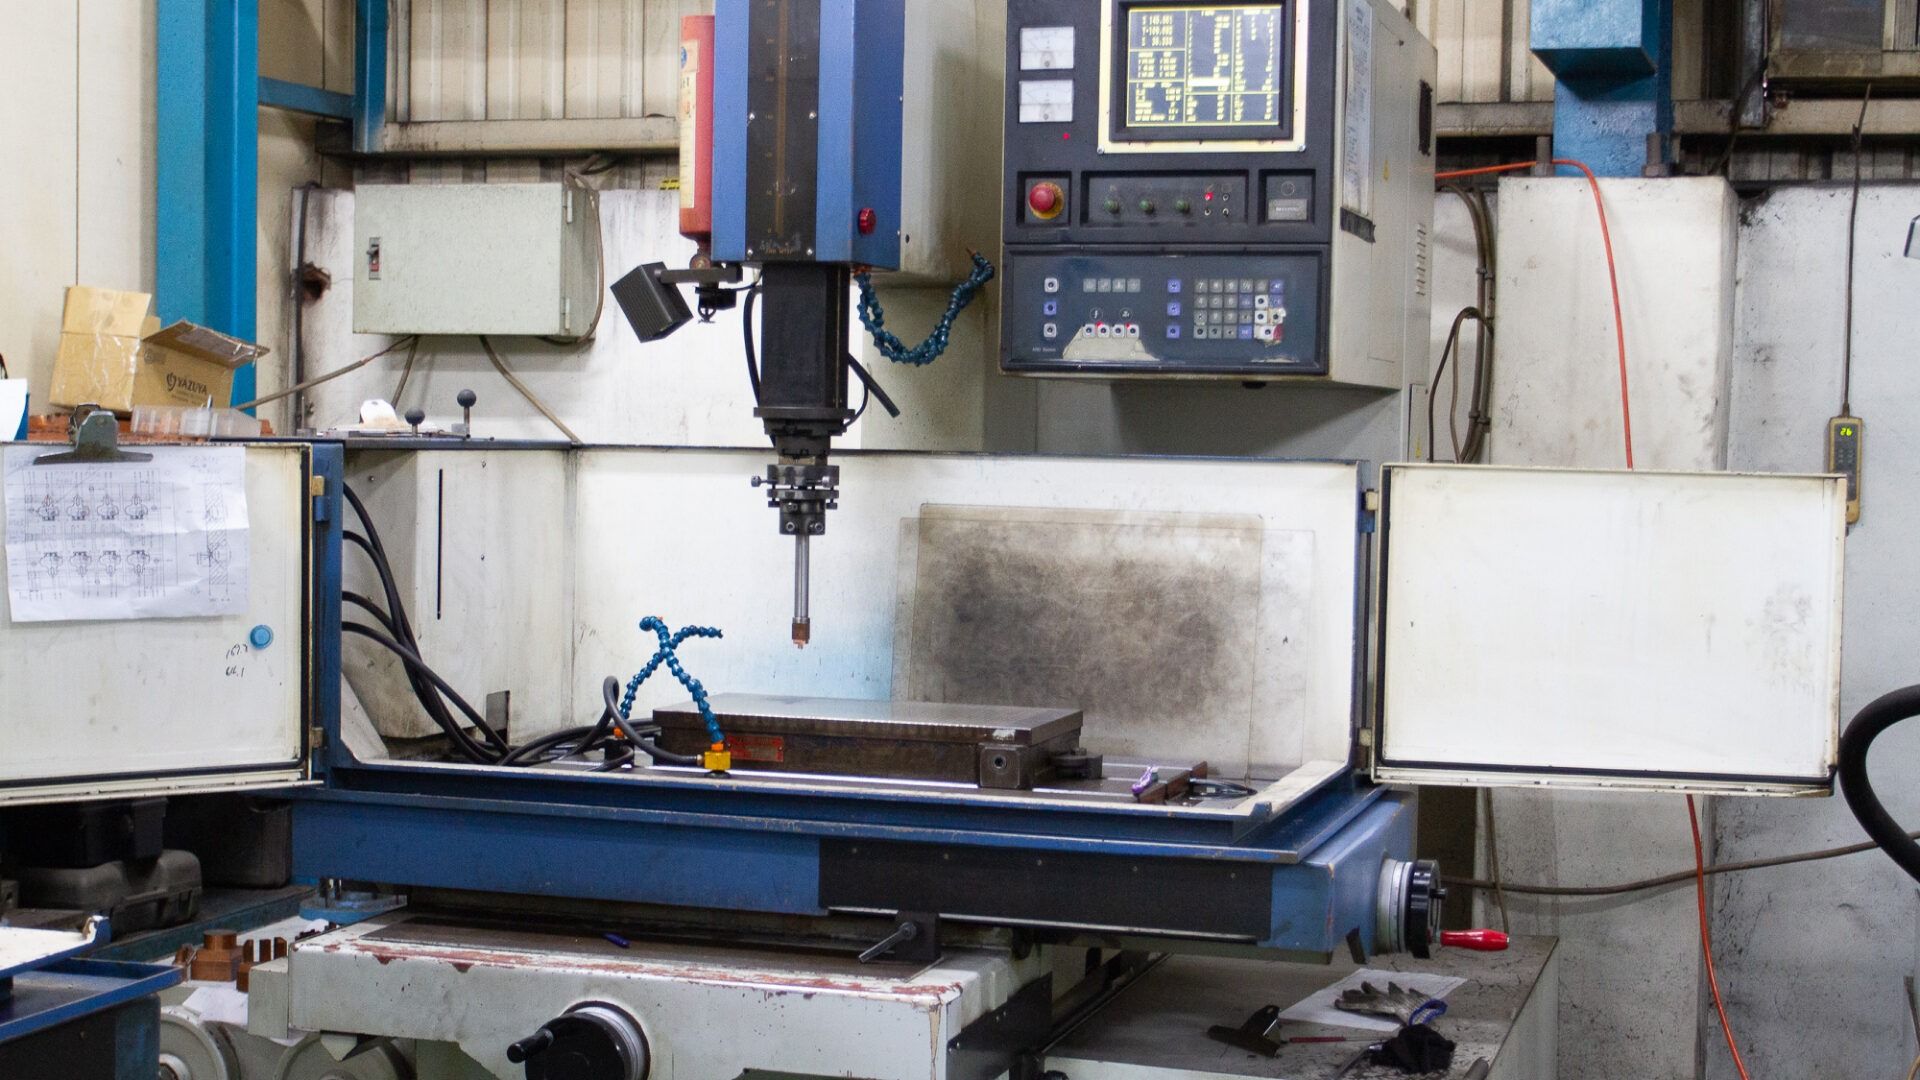
EDM machine 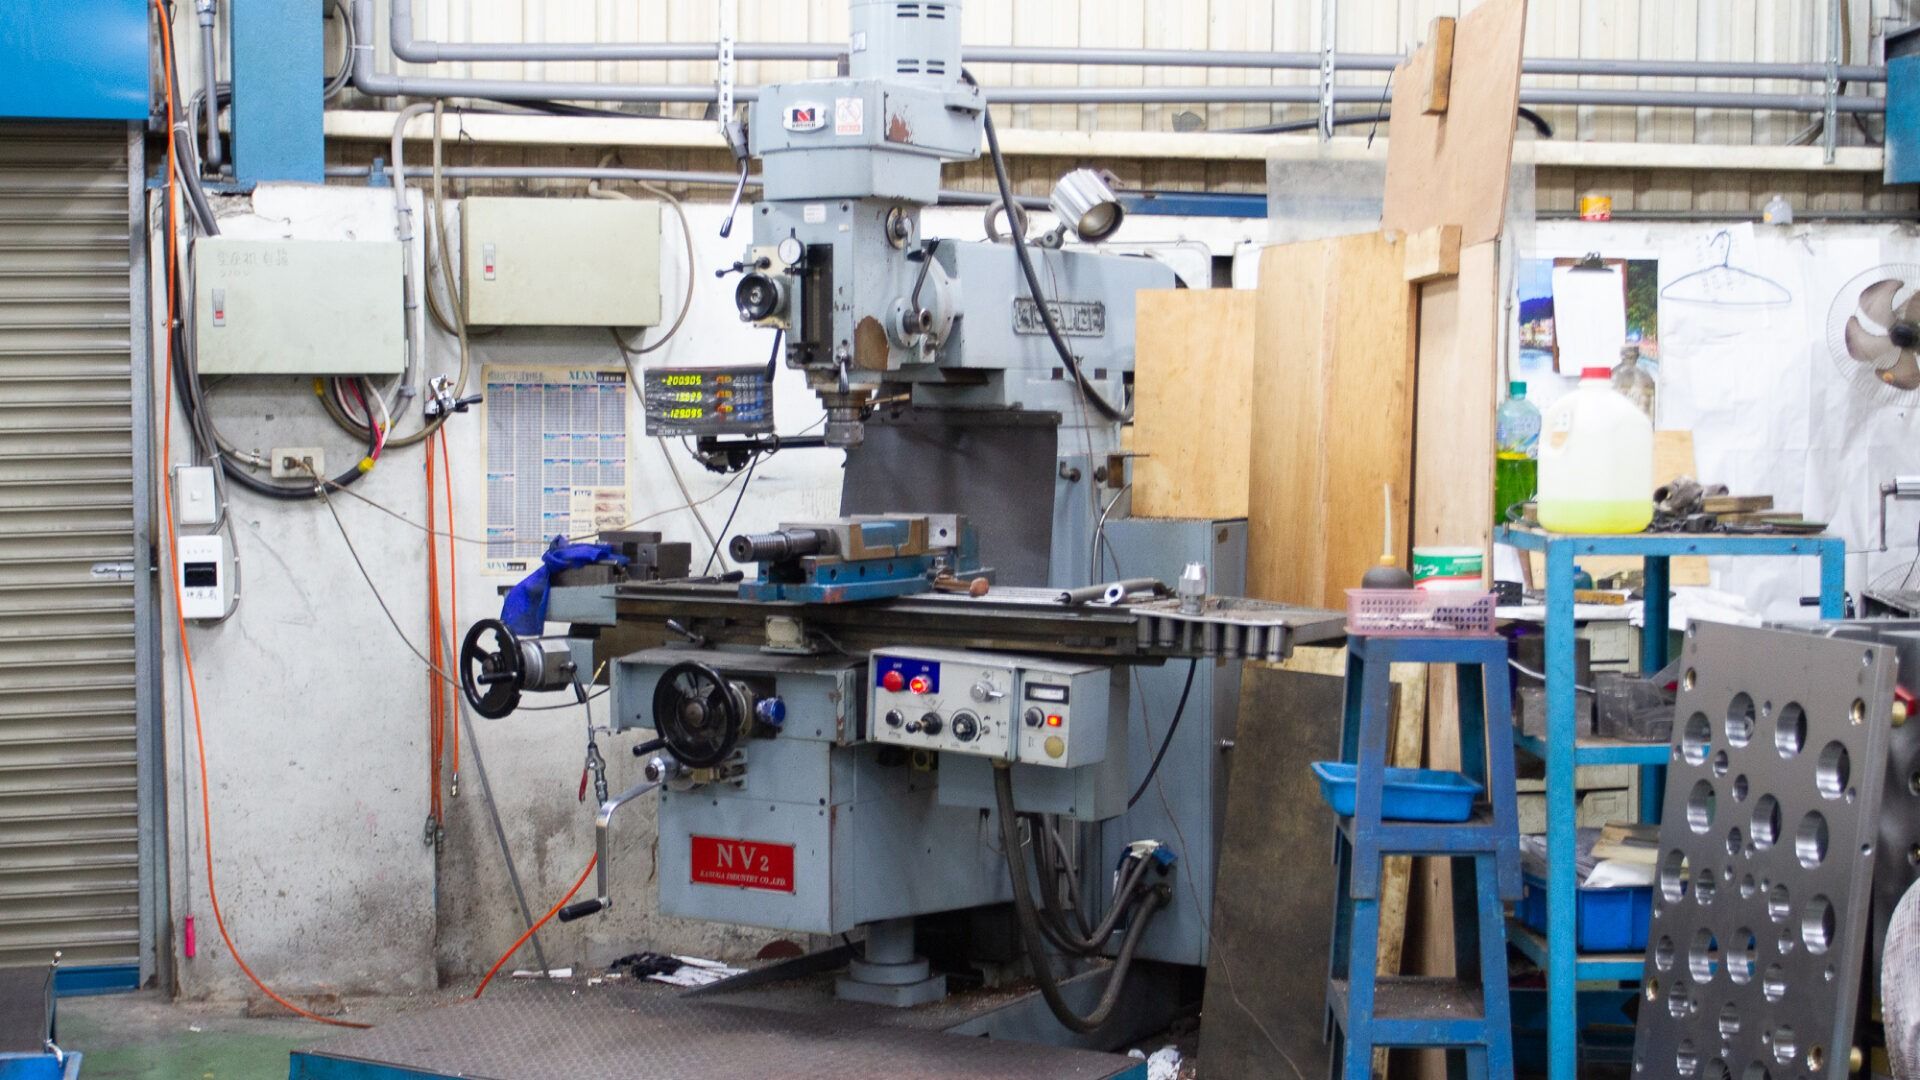
Milling machine 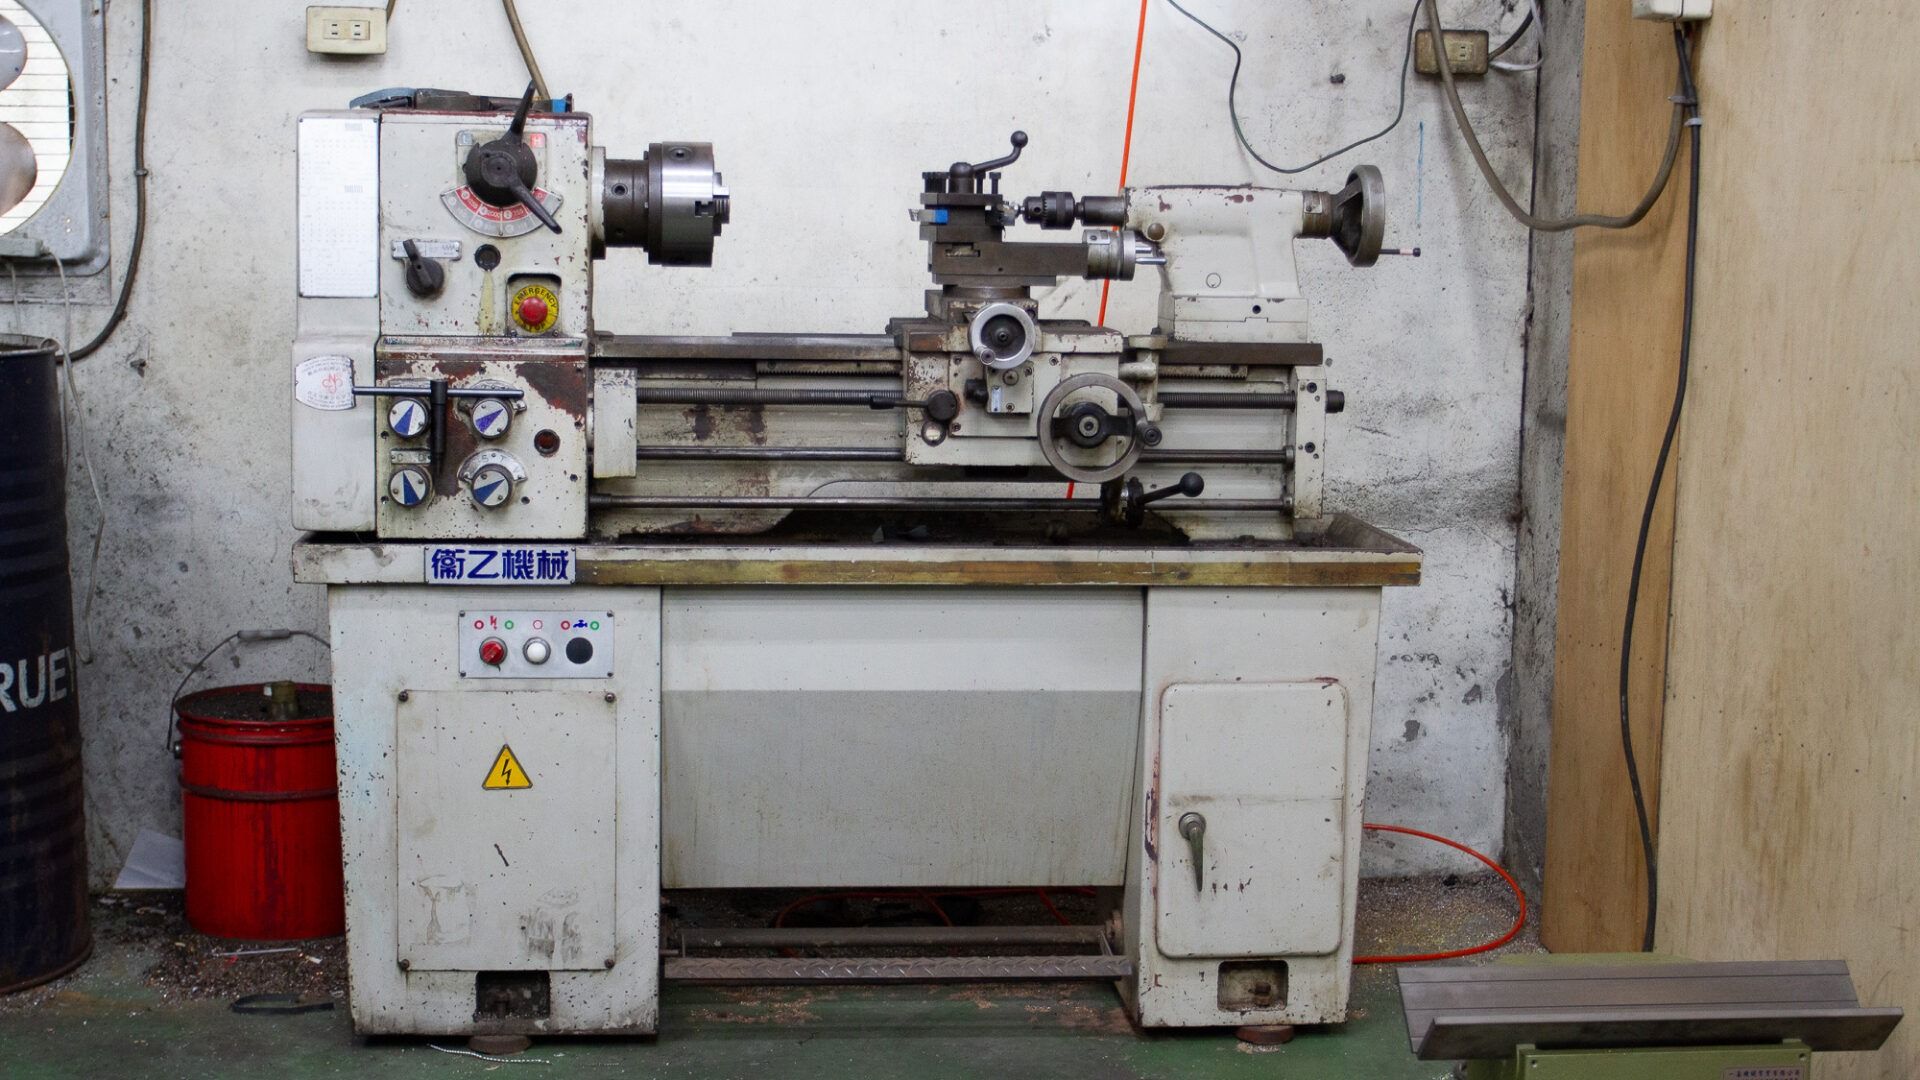
Lathe 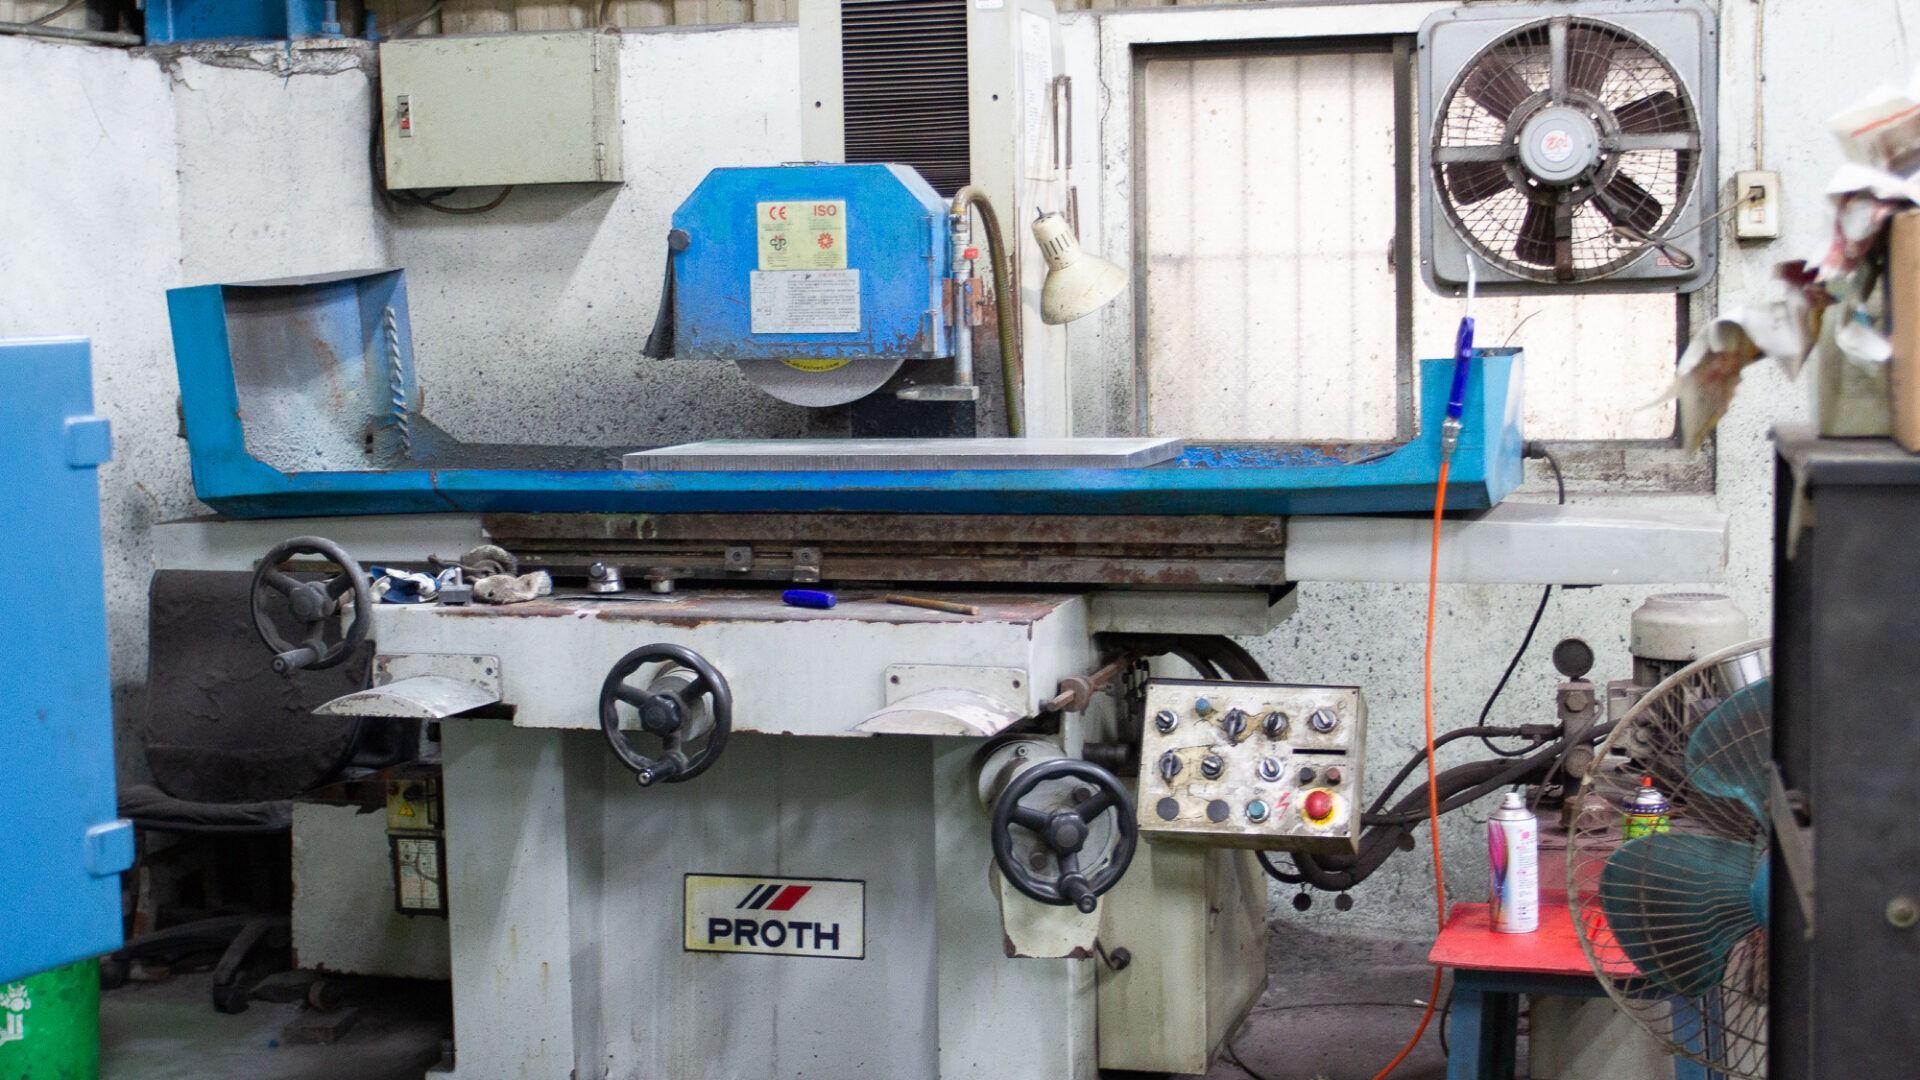
Surface grinder
04 / Trial presses
Trial presses: which press fits your mold
Finished molds are tried out on Chang-Hao’s own presses. Besides press tonnage, the mold has to fit between the tie bars and its thickness must fall within the press’s mold height range; the table lists these figures for each press.
All press specifications| Press tonnage | Presses | Tie-bar spacing (mm) | Mold height (mm) | Opening stroke (mm) |
|---|---|---|---|---|
| 80 t | 1 | 410 × 360 | 150 to 380 | 320 |
| 100 t | 2 | 410 × 410 | 150 to 430 | 360 |
| 140 t | 1 | 460 × 460 | 150 to 450 | 400 |
| 180 t | 1 | 510 × 510 | 200 to 500 | 470 |
| 260 t | 1 | 615 × 615 | 250 to 700 | 580 |
| 280 t | 1 | 605 × 605 | 250 to 650 | 580 |
| 500 t | 1 | 820 × 820 | 300 to 900 | 800 |
| 850 t | 2 | 1,100 × 1,000 | 500 to 1,200 | 1,025.5 |
FAQ
Mold making questions
- Where are Chang-Hao’s molds made?
- In Chang-Hao’s own tool room, which has EDM, milling, turning and surface grinding machines.
- What steps does a new mold go through?
- 12 steps: quotation, kickoff meeting, mold design, production plan, material and drawings, machining, mold fitting, mold trial, corrections, quality inspection, mold complete and shipment.
- Where are new molds tried out?
- On Chang-Hao’s own presses. Chang-Hao merged its molding plant and mold shop in 2000 and has 10 presses from 80 to 850 tons.
- What is a weld line?
- The place where two flow fronts meet during injection. Autodesk Moldflow notes that weld lines are unavoidable when the flow front splits and comes together, around a hole, or with multiple gates.
Send a sample or drawing for a quote
Please send a sample or drawing of your part. We confirm the details and then send a quote.